Paperboard Chain of Custody Certificate Verification Basics
Verify paperboard claims by checking the online scheme register, matching scope codes, and auditing transaction lines on invoices and delivery dockets.
Verify paperboard claims by checking the online scheme register, matching scope codes, and auditing transaction lines on invoices and delivery dockets.
Dynamic platen converting above 7,500 sph degrades board core shear modulus by up to 60 percent, demanding calibrated matrix tooling to prevent carton collapse.
Integrating real-time scanner defect maps into multi-machine slitting formulations eliminates downstream press downtime by dynamically routing edge flaws into trim.
Dynamic stiffening at rotary converting speeds forces delamination failure modes, requiring tuned counter clearances to protect outer carton liners from rupture.
Chemithermomechanical core compliance modeling predicts time-dependent box compression decay under changing humidity by coupling viscoelastic Prony series with shear kinematics.
Inline ultrasonic testing verifies internal score delamination and folding resistance in real time, preventing visual surface cracking and high-speed erect jams.
Calculate matrix channel width for co-extruded laminates using an expanded 1.65 to 1.85 board modifier plus rule gauge and double film thickness.
Jet-to-wire velocity ratios govern machine-direction fiber orientation, setting board anisotropy ratios that dictate box compression and score crack resistance.
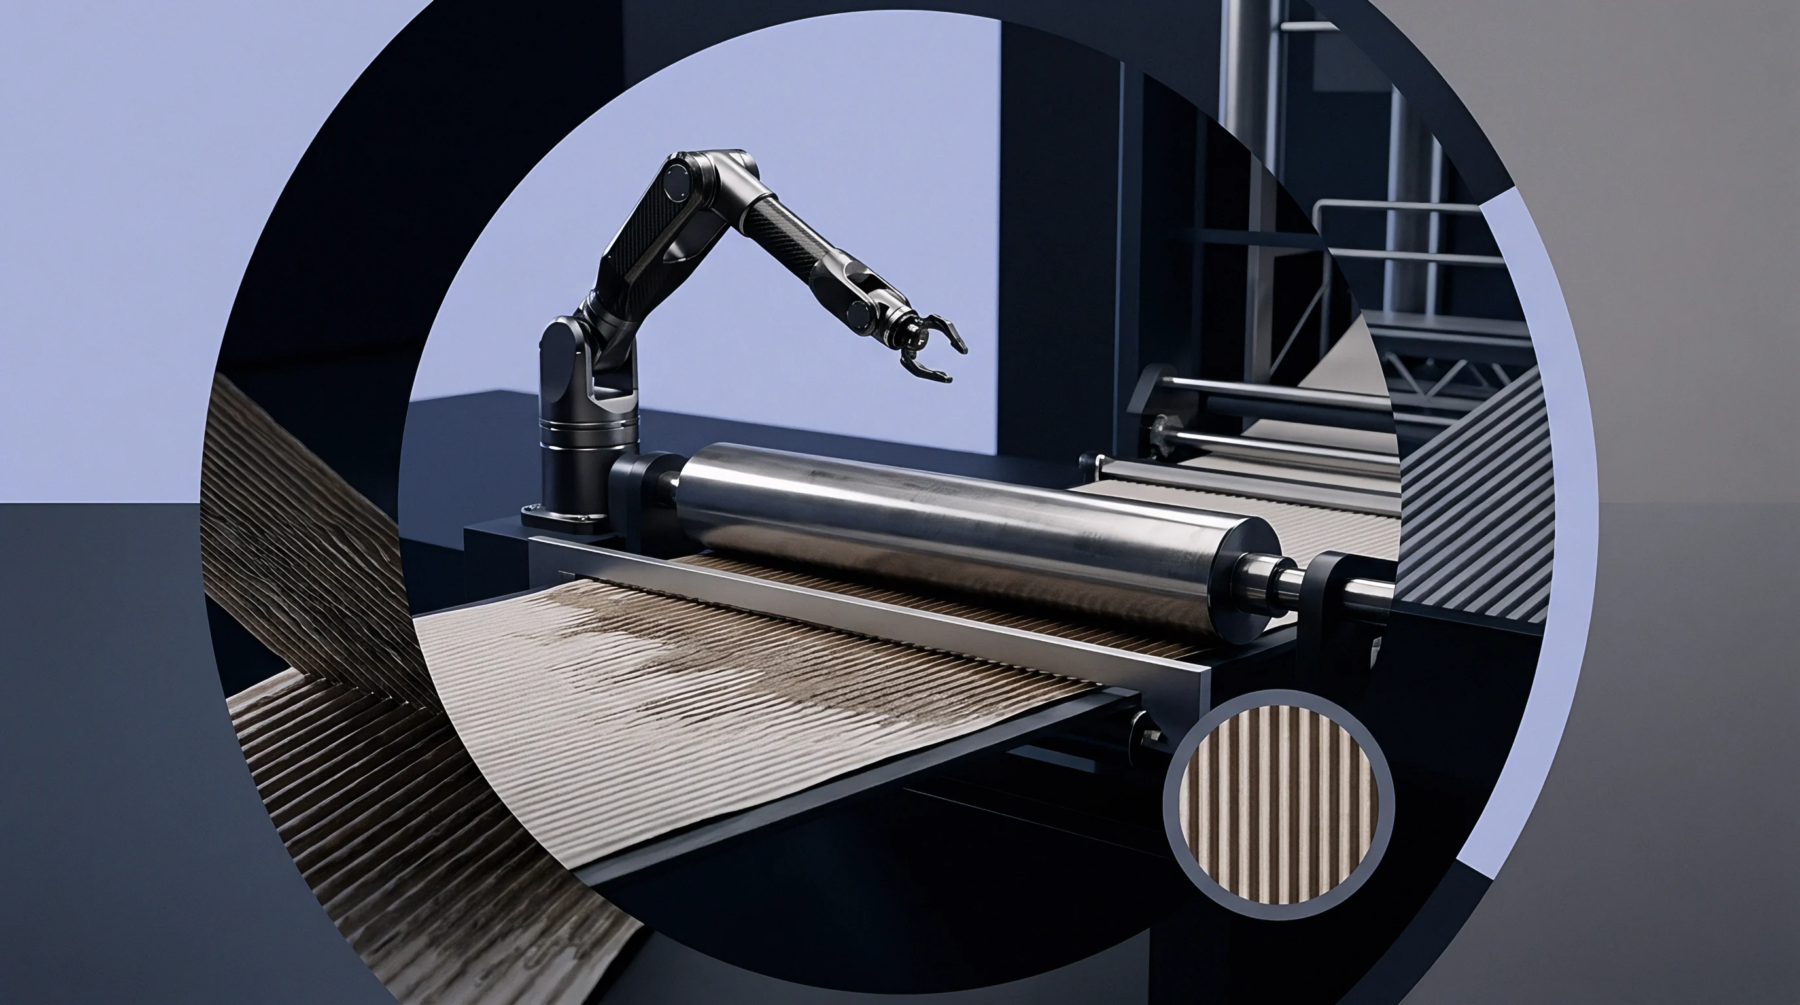
Cross-machine caliper control demands real-time induction calender profiling to maintain stiffness and prevent high-speed converting line jams.
Validating paperboard claims requires cross-checking certificate scope codes on public databases and securing batch migration test reports.
Foil adhesion succeeds when polymer film surface energy exceeds forty-two dynes per centimeter and sizing chemistry matches the polar surface component.
Swapping dense SBS for bulky FBB preserves bending stiffness through thickness retention while cutting material weight by fifteen to twenty percent per carton.
Paperboard moisture verification demands ISO 186 random lot sampling and preconditioning under ISO 187 before ISO 287 gravimetric testing.
Verify paperboard certificates by matching invoice claim text, product scope codes, and valid supplier registry entries before receiving inventory at the dock.
Optimizing folding boxboard stiffness requires balancing BCTMP core bulk with chemical pulp outer layers to maximize moment of inertia at target carton speeds.
Landed sheet cost calculations require combining imposition trim, setup spoilage, moisture-adjusted mass, tare deductions, and scrap credits per unit.
Paperboard fiber ratio auditing requires pairing ISO 9184 Graff C microscopic stain counts with EN 16995 chemical marker testing and mass-balance credit ledgers
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.